Copyright © 2026 J and E Engineering Services Ltd All Rights Reserved

J and E Engineering Services Ltd.
Unit 32 Britannia Mill,
Stoneholme Road,
Crawshawbooth,
Rossendale,
Lancashire.
BB4 8BA.
Monday
Tuesday
Wednesday
Thursday
Friday
Saturday
Sunday
8:30am -
8:30am -
8:30am -
8:30am -
8:30am -
9:00am -
Closed



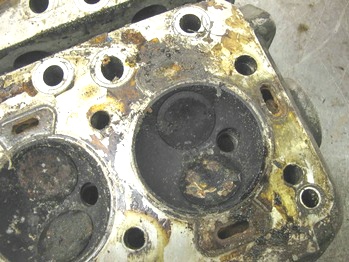
On this page we will discuss how we rebuilt the cylinder heads for the Daimler V8 from start to finish. We will discuss the upgrades and modifications included in our standard specification heads and show you some of the issues that you may come across when rebuilding your cylinder heads.
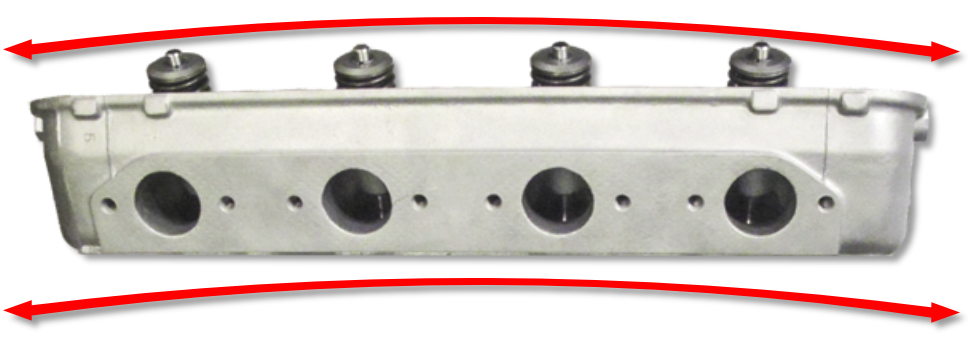
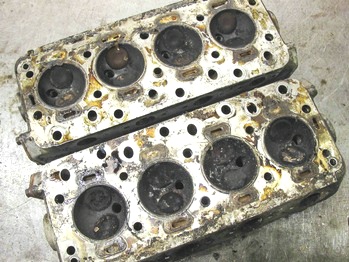
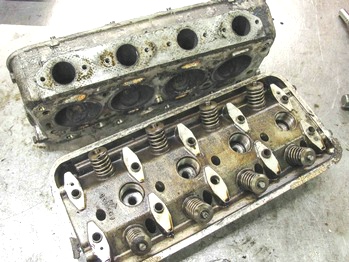
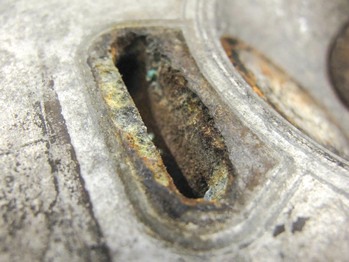
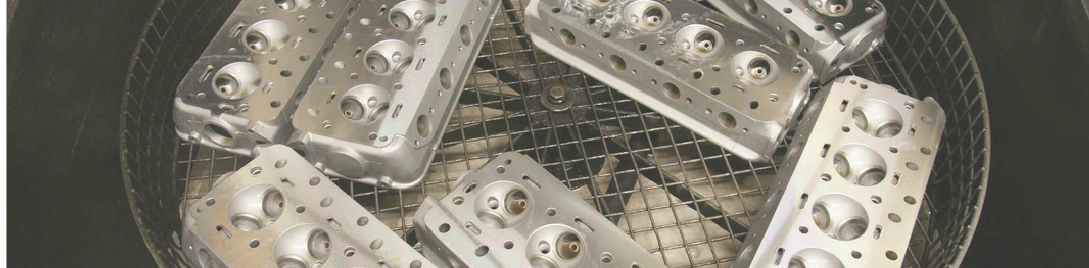
A typical pair of cylinder heads showing various issues from leaking core plugs, burnt out valves to warping &corrosion. First an initial inspection strip down & 1st stage clean & degreasing of the castings is required this makes any issues easier to spot. Spark plug tubes and any dowels are removed at this point. Valves are discarded as they will be replaced, springs, collets, caps & seats are retained for checking & re-
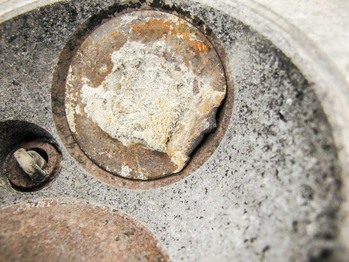
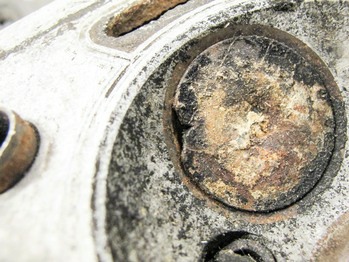
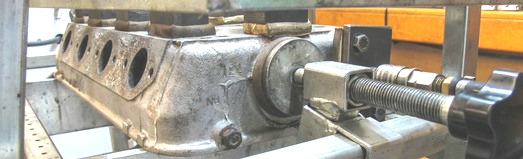
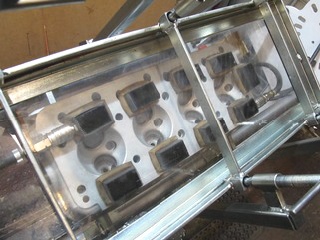
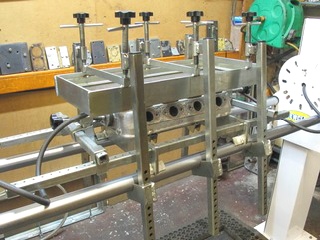
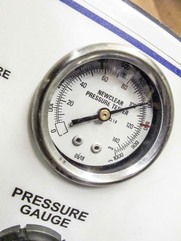
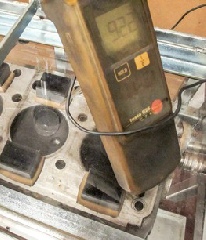
A three stage pressure test at over 60psi will show if the cylinder head has a casting defect in the form of porosity or a crack.
The three test stages are: Air, Hydraulic & Hot Hydraulic.
Leaks from the core plugs are common and these are replaced with a cup type modification as part of the rebuild, so no concern at this stage. If the cylinder head passes this stage we can move on to the next.
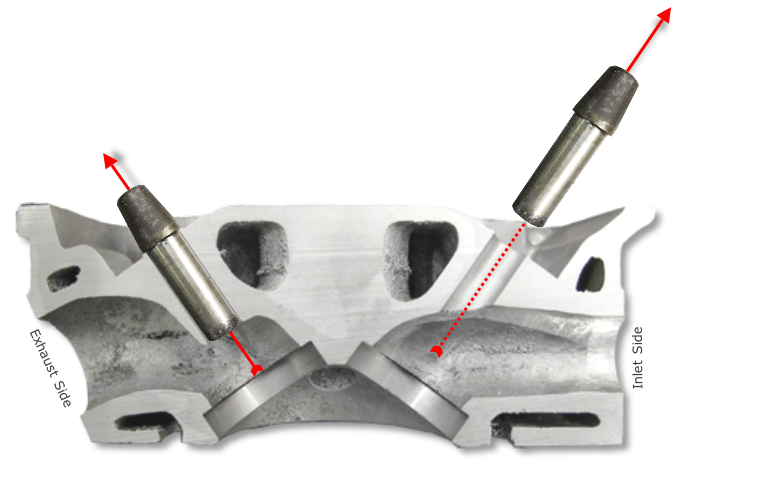
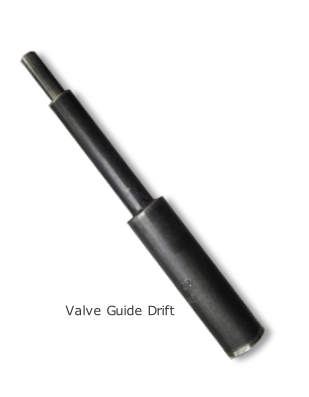
The old valve guides are to be replaced as part of the essential valve stem oil seal modification. These are simply knocked out using a suitable drift of the correct size. The guides can only be removed in one direction as they have a stepped register on the rocker shaft side.
 Pressure Testing Additional Info
With the valve guides removed the bare casting is subject to an intensive de-
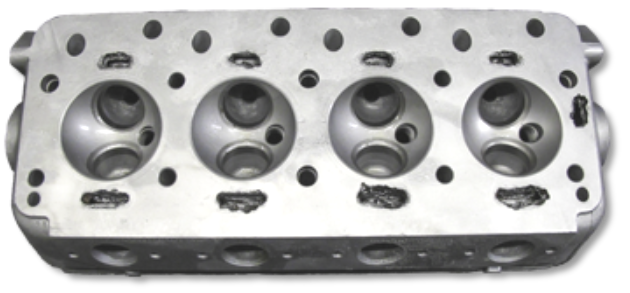
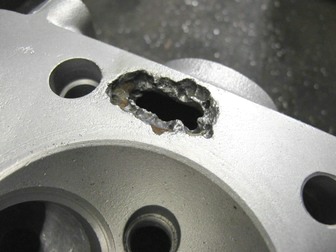
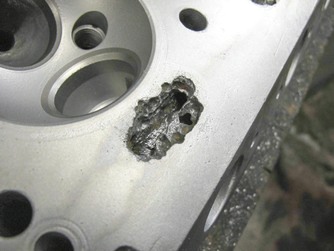
Coolant passage corrosion can be a real problem and is not uncommon. This problem can only be repaired by welding. Replacing bad metal with good.
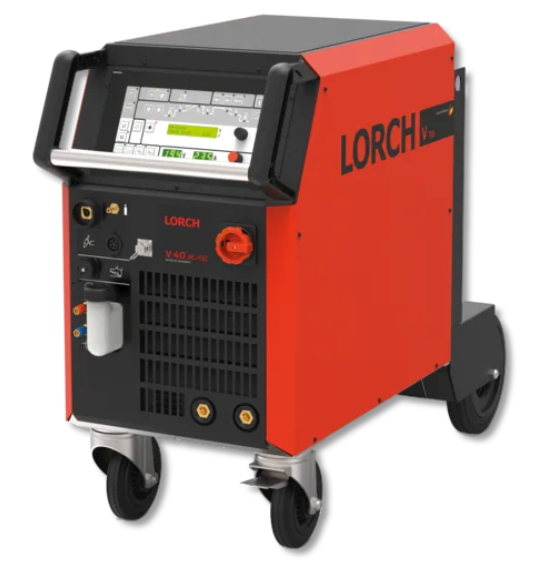
We ‘tig’ weld our corroded cylinder heads using a specialist 4943 aluminium filler rod. We do not use any chemical resins, composites, cold weld or liquid metal fillers, just aluminium plain and simple. Our V’series, Lorch welding machine allows us to get welding quickly without a reliance on an extensive pre-
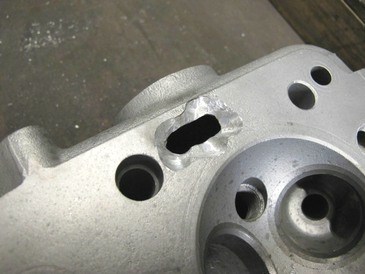
The corroded material & contamination is removed with a carbide burr and die-
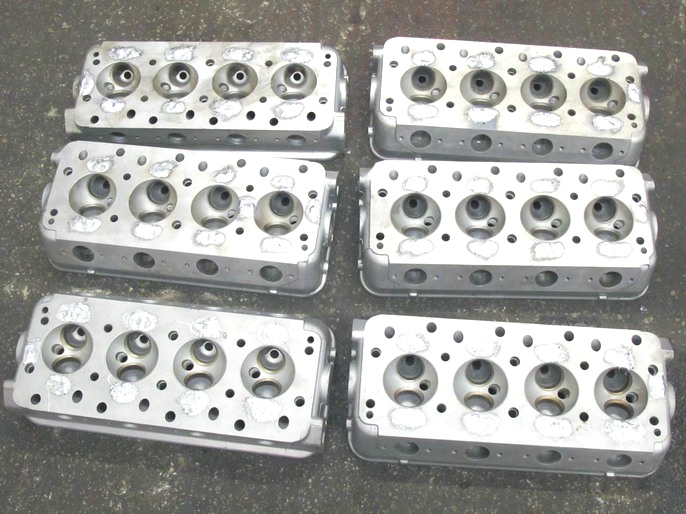
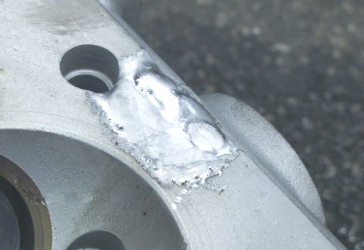
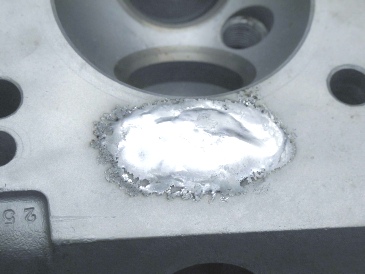
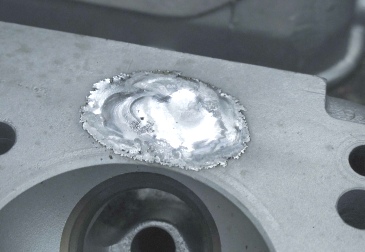
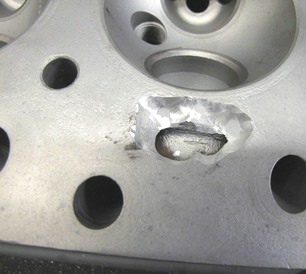
Here a batch of Daimler V8 cylinder heads can be seen after the welding phase has been completed. You will notice the coolant passages completely welded. This will by rectified in the next operation.
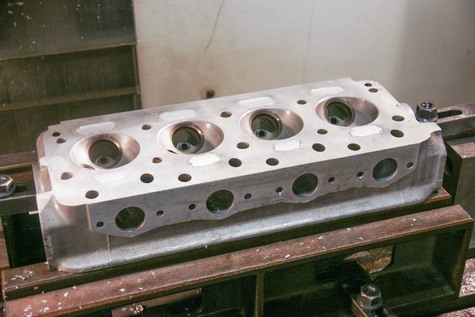
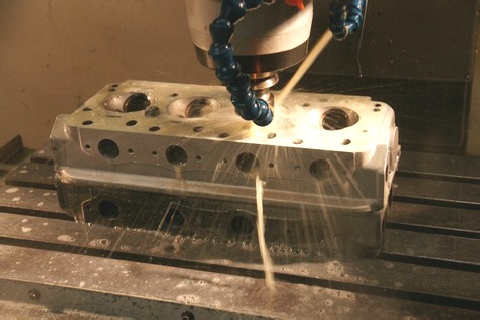
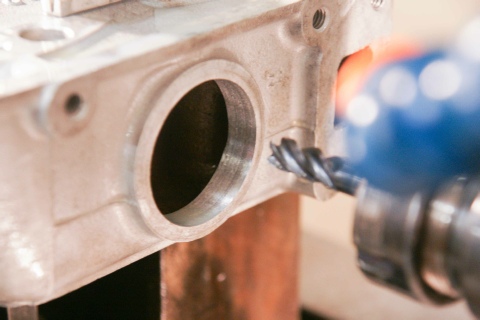
The welded cylinder head is mounted onto the CNC milling machine and zero position set. A pre-
Aluminium welding, un-
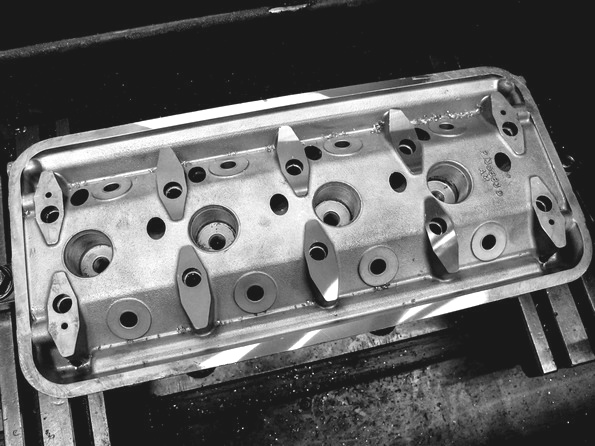
The image left shows the top face of the cylinder head during the machining process. You can see where the middle six rocker pedestal platforms and rocker cover sealing edge has cleaned up. The outer parts remain below the machined level proving the diagram shown above is correct and that the cylinder head is indeed distorted (Warped) on this face. Any rocker shaft which is fitted to a cylinder head like this will follow the same distortion and conform to it by bending. This can lead to sticking rocker arms, accelerated wear and shaft fracture in extreme cases. Sticking rocker arms can be identified by tapping or knocking noises when running, similar to a tappet noise but one which cannot be silenced by adjusting the clearances.
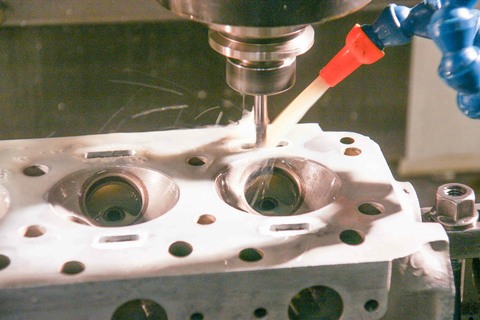
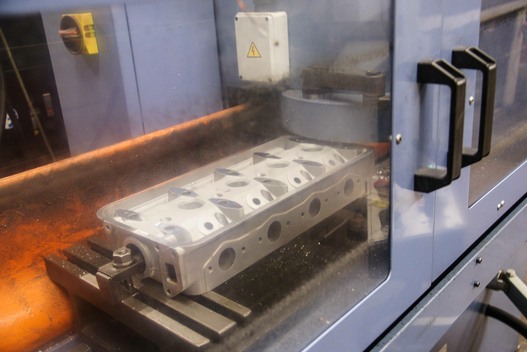
The cylinder head can only be machined on this face with the valve guides removed as they protrude above the face when fitted. All our fully rebuilt cylinder head castings are machined in this way using PCD diamond tooling as seen below.
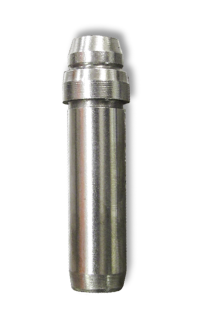
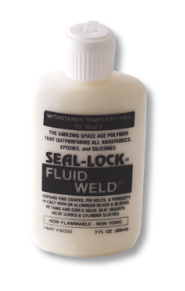
With the top face fully machined we can now fit the new, modified valve guides. The guide bores in the cylinder head are measured for size and any oversize holes can be fitted with an oversize guide. We press the guides into place using a female drift that protects the top of the valve guide. A special adhesive is also applied to act as first a lubricant to prevent galling and second to retain the guide in the head. The guides are pressed in until the top register contacts the cylinder head. Remember the inlet valve guide is slightly longer than the exhaust valve guide.
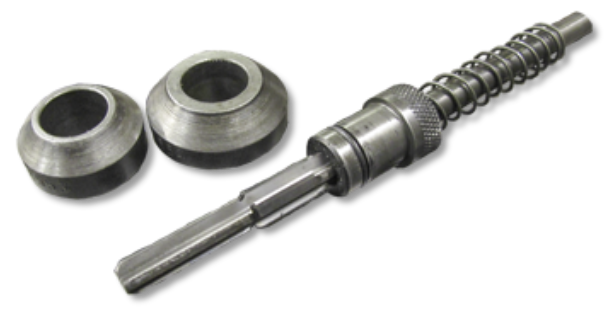
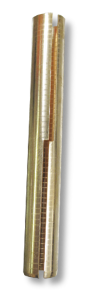
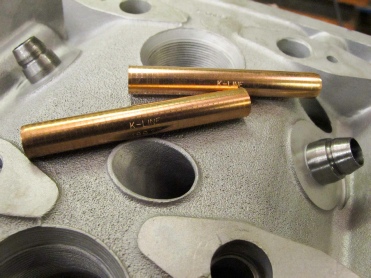
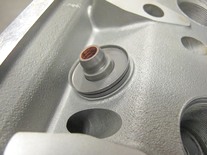
Once the new guide is in place it is modified further with the adding of a genuine K-
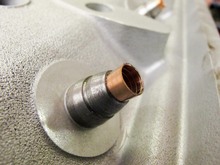
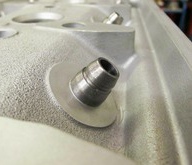
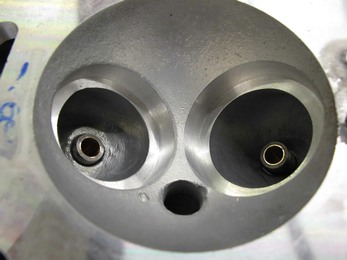
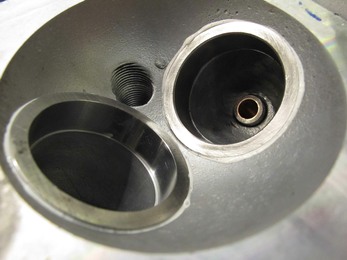
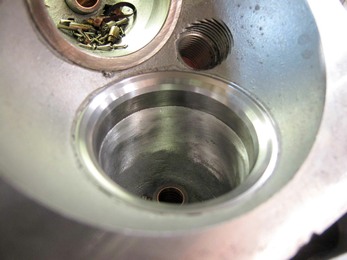
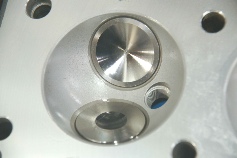
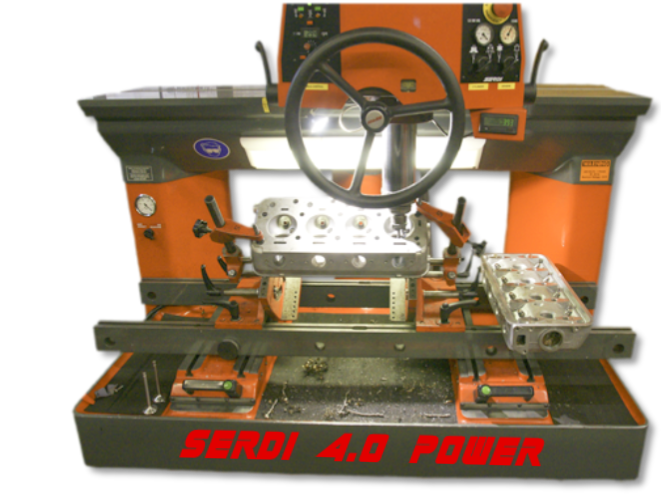
With the new valve guide in place and correctly sized we can now cut the valve seat concentric, round and true. For this we use a dedicated seat and guide machine the Serdi 4.0 Power. The machine uses a live pilot and adjustable carbide cutting tip centralised by a triple air floating system to ensure accuracy. Valve seat cut in this way do not require lapping with grinding paste and sucker sticks.
Fortunately the seats used in production By Daimler and Jaguar are suitable for unleaded fuel and do not require replacement under normal circumstances. Valve seats do sometimes require replacement when severe wear, excessive cutting or other damage has occurred. We use a special ‘Hi-
Above you ca see a valve seat replacement process as & when required. Old seats removed, new seats fitted followed by final seat re-
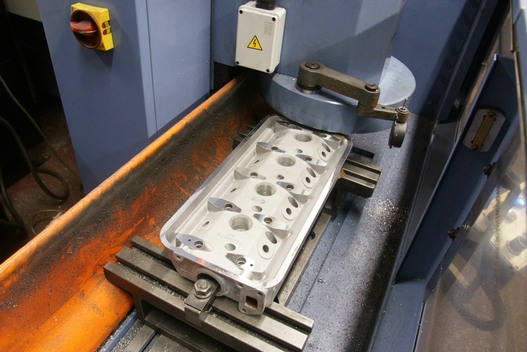
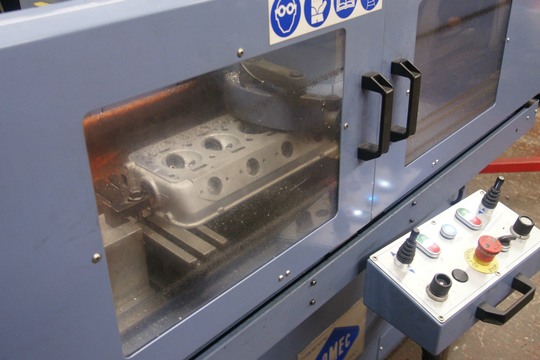
With seat cutting complete we can now machine the cylinder head gasket face flat & true. We do this as the last machining operation because the surface finish is of critical importance and the other operations could damage the face. The images directly below show the surface milling machine in action and a cylinder head with warp and distortion clearly visible.
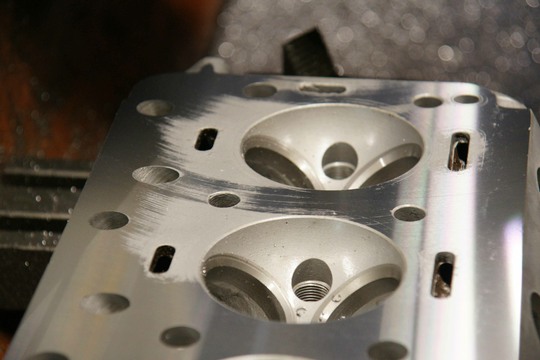
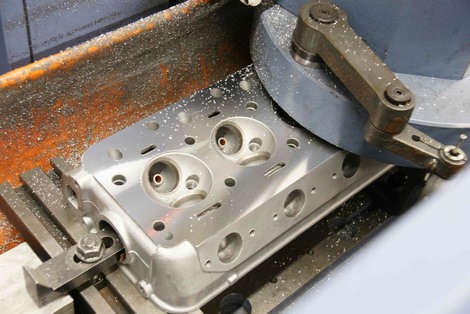
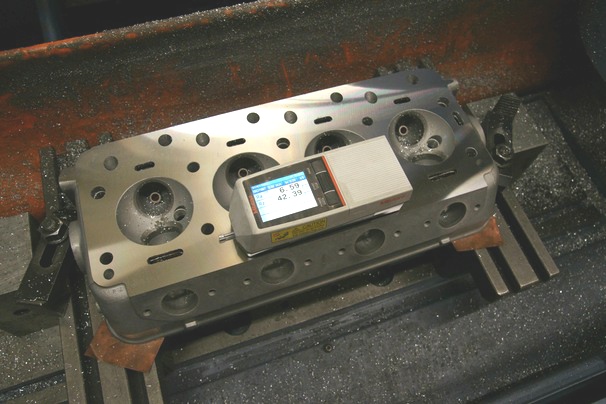
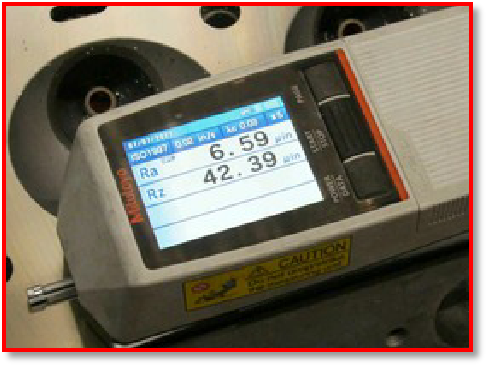
After machining the surface roughness is checked to ensure it is smooth enough for the single layer steel (SLS) cylinder head gasket. This type of gasket requires a roughness average (Ra) of less than 30µin (Micro inches). As you can see our diamond tipped machining can produce a finish of under 10µin (Micro inches). The holes are then chamfered and de-
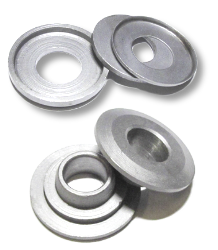
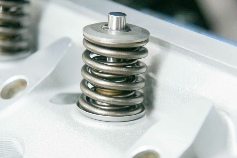
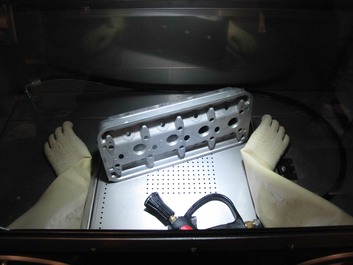
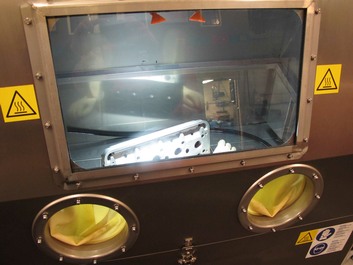
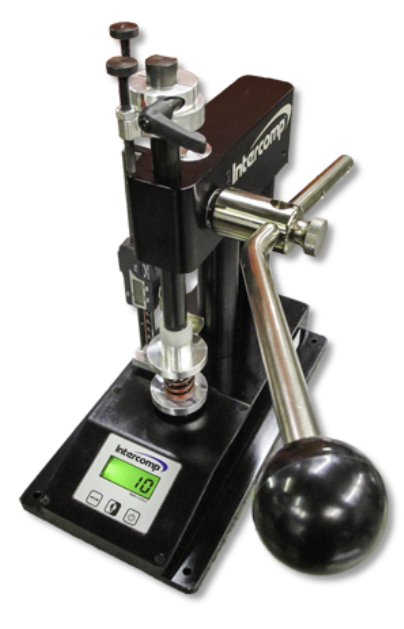
Valve retaining caps, collets, valve spring seats are all cleaned thoroughly by vapour blasting. Valve springs are checked for seated pressure and full lift weights using our dedicated spring test machine. The standard install height of the spring should be 33.27mm with a seating spring pressure of about 60lb. Any springs which do not make the grade are replaced. Our uprated spring set offers a seating pressure of 82lb and a full lift pressure of around 140lb. These pressures can be tweaked with different combinations of spring seats and shims.
The cylinder heads can now be assembled complete with modified & uprated valve stem oil seals and modified core plugs. New oil blanking plugs with sealing washers are also fitted. Once assembled valve seating is checked using a vacuum generator.
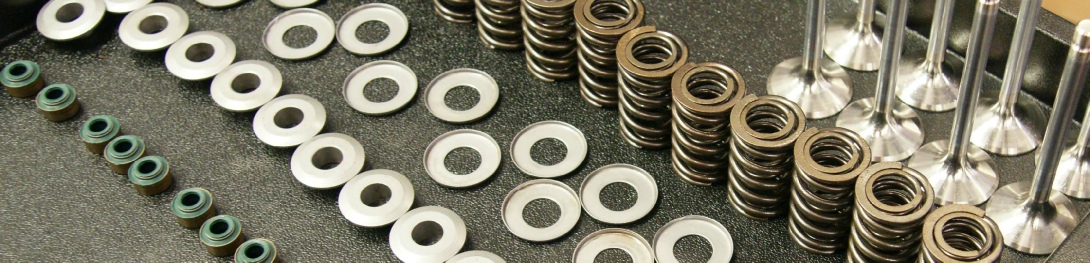
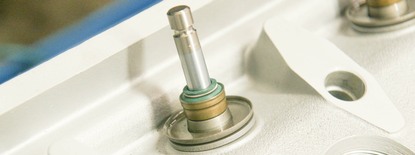
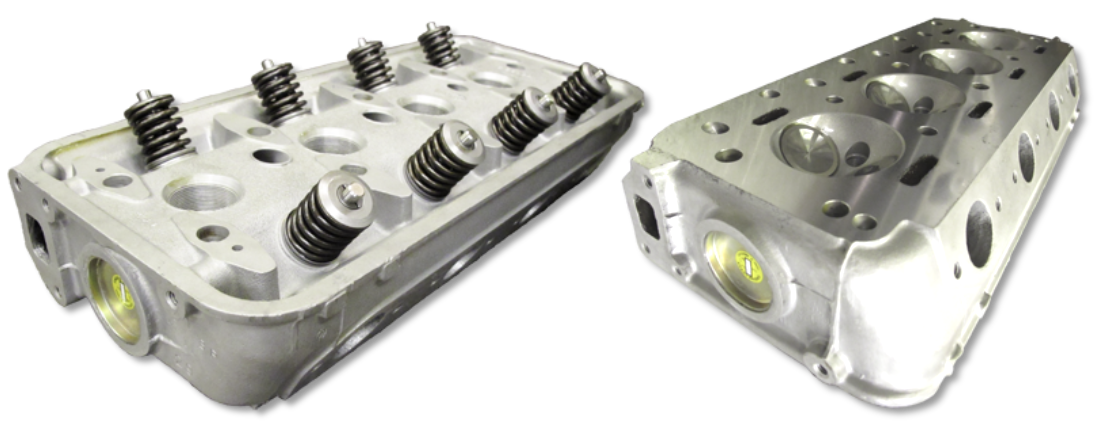
All J & E Engineering rebuilt cylinder heads are built to the same specification detailed below.
3-
Spark plug tube removal, manifold stud removal, thread inspection & repairs.
Full chemical de-
Vapour Honed cylinder head castings. x2
Aluminium welding repairs to corroded areas. (If required).
CNC machining of coolant passage slots. (If required).
Cup type core plug modifications to both ends of head. X4.
Valve seat replacement. (If required).
Machining of rocker pedestal & rocker cover top face.
New modified valve guides. x16.
Genuine K-
Viton uprated valve stem oil seals. X16.
New intake valves. x8.
New exhaust valves. X8.
New uprated valve spring set. (If required).
Intake & exhaust valve seats re-
Vapour honed valve retainers, collet pairs & spring seat platforms.
Cylinder head gasket face fly-
Thickness measured & recorded for data sheet.
Oil passage blanking plug & sealing washer. X4.
Cup type core plug fitting. X4.
Assembly.
Valve seating vacuum checks & other QC checks.
Temperature tell-
Complete data & rebuild sheet supplied with each pair of heads.